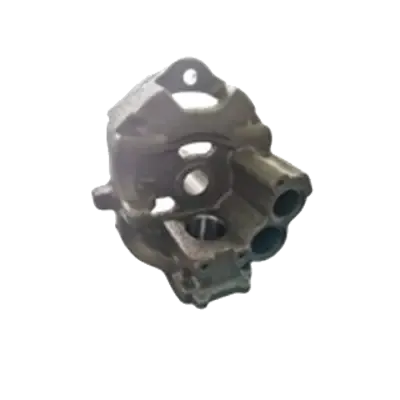
Crank Case (Type 2)

A complete honing solutions under one roof

Request a Quote

Crank Case (Type 2)

Crank Case With A Precision Finished Bore

Advancements

Manufacturers are continually pushing the envelope in regard to what can be accomplished with the single pass Honing Process. Improved tool, fixture and machine designs have allowed for increased production rates as well as improved bore precision. The following are some of the latest advancements that have been made.

Through Bore

The key to the single pass Process is to allow the diamond tooling to follow the existing centreline of the bore to be finished with as little pressure as possible. This is normally done by allowing the part to float along with the fixture to achieve the bore sizes and geometry.
Case History : 21

Data table: Material, Cast Iron, Hardness, 180 TO 220 BHN
MaterialCast IronHardness180 TO 220 BHN
Bore TypeThrough BoreStock Removal50 to 55 Micron
I/P SizeØ30.117Length35 mm
Tool 1Ø30.132GritBU
Tool 2Ø30.145GritBU
Tool 3Ø30.154GritBS
Tool 4Ø30.160GritBO
Tool 5Ø30.163GritBM
Tool 6Ø30.167-Burnishing Tool
Data table: BORE DIMENSIONS, REQUIRED, ACHIEVED
BORE DIMENSIONSREQUIREDACHIEVED
SizeØ30.167 (±0.005)Ø30.168/Ø30.169
Perpendicularity0.009 mm0.003/0.005 mm
Surface Finish0.3 Ra0.2 Ra
Data table: Machine Type, ABS 608 (8-Spindle 6-Station)
Machine TypeABS 608 (8-Spindle 6-Station)
Cycle Time16 Sec/Component
Production220 Nos/Hour

Let's start creatingtogether

Phone