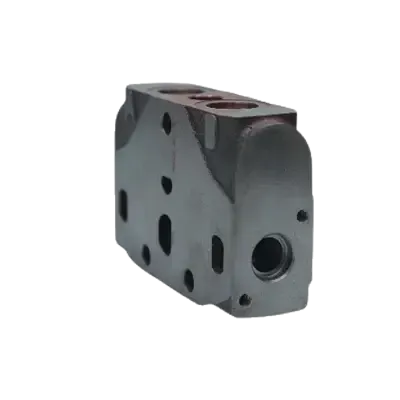
Hydraulic Valve (Type 1)
Advancements
Manufacturers are continually pushing the envelope in regard to what can be accomplished with the single pass Honing Process. Improved tool, fixture and machine designs have allowed for increased production rates as well as improved bore precision. The followings are some of the latest advancements that have been made.
Cost Reductions
The following case histories are good examples of where component manufacturers were able to improve bore quality and dramatically reduce costs by switching from the conventional process to the single pass Honing Process. More and more manufacturers are now switching over to the single pass Process for this operation and realizing cost savings as much as 50%.